 View Product ↗
01
Product Description
Technical details, material information and manufacturing notes for this product.
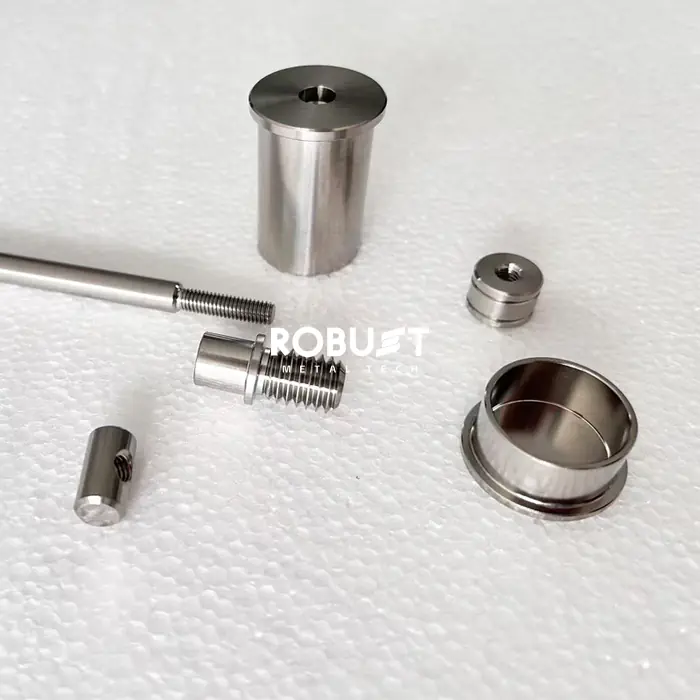
1. Primary Machining Technologies
The choice of process depends on the part's symmetry and complexity.
Process | Best For | Capabilities |
CNC Turning | Cylindrical parts, shafts, bushings | High-speed rotation, excellent concentricity |
CNC Milling | Prismatic parts, housings, brackets | 5-axis movement for complex 3D contours |
Wire EDM | Ultra-thin slots, sharp internal corners | Stress-free cutting of hardened titanium |
Swiss Machining | Micro-parts (screws, pins) | High-volume, small diameter precision |
2. Select the Right Grade
Grade | Type | Characteristics | Best For |
Grade 2 | Commercially Pure | Highly ductile, excellent corrosion resistance. | Chemical processing, marine parts. |
Grade 5 | Ti-6Al-4V | The "workhorse." High strength, heat treatable. | Aerospace, medical implants, racing. |
3. Design for Manufacturability (DFM)
Machining titanium is more expensive than steel or aluminum; smart design can significantly lower costs.
Avoid Deep Pockets: Tools can vibrate (chatter) in deep cavities. Keep depth-to-width ratios below 4:1.
Large Internal Radii: Tiny corner radii require small, fragile tools that break easily in titanium. Use the largest possible radius.
Thread Depth: Titanium is so strong that threads deeper than 2x the diameter add little strength but significantly increase the risk of tap breakage.
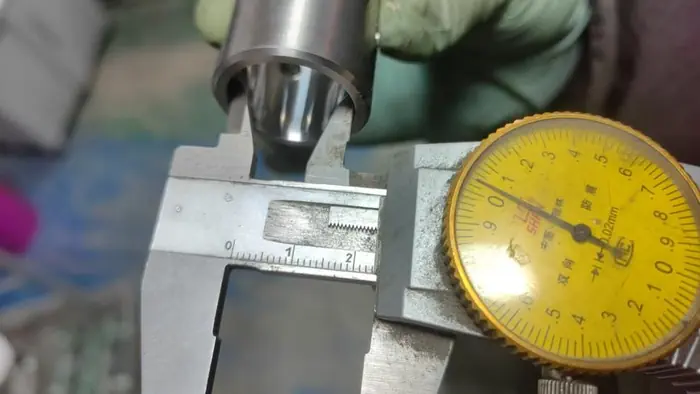
Wall Thickness: Maintain a minimum wall thickness of 0.5 mm to prevent the part from warping due to machining heat.
4. Surface Finishing Options
Post-machining treatments enhance both the performance and the appearance of the part.
Anodizing (Type II & III): Increases wear resistance and provides color coding (Type II) or a thick, protective grey oxide layer (Type III).
Passivation: A chemical treatment that maximizes the natural protective oxide layer for medical or high-purity use.
Bead Blasting: Provides a uniform, matte "satin" finish and hides tool marks.
Electropolishing: Removes microscopic surface peaks to create a mirror-like, ultra-clean surface.
PVD Coating: (Physical Vapor Deposition) Adds an ultra-hard layer (like TiN) to increase surface hardness and reduce friction.
04
Related Technical Resources
Material guides, application notes and manufacturing knowledge from ROBUST.
05